Laser Cutting Stainless Steel Type
Not all stainless steel is the same. When selecting a material suitable for laser cutting, it is important to consider the type of stainless steel to be used. Some grades are easier to cut than others, and each has unique properties that can affect the cutting process.

Laser cutting is currently one of the most common methods for processing 304/316 stainless steel. Industrial fiber laser cutting machines (ranging from 1,000 W to tens of thousands of watts) can easily cut stainless steel sheets ranging from a few millimeters to tens of millimeters in thickness. An ultra-high-power laser of 20,000 W (20 kW) can even cut 304 stainless steel up to 40 mm thick.

430 stainless steel has better thermal conductivity than austenitic stainless steel. This makes it melt more efficiently during laser cutting, allowing for slightly faster cutting speeds at the same power level. Fiber laser cutting machines have an extremely high absorption rate for stainless steel. When processing thin sheets of 1–3 mm, a power range of 1,000 W to 2,000 W can achieve high cutting speeds of 30–80 mm/s, with precise cuts and tight tolerances.

2205 duplex stainless steel has a high alloy content, and its thermal conductivity and melting characteristics differ from those of ordinary austenitic stainless steel. Taking the cutting of 12-mm-thick sheet metal as an example, when using an 8-kW fiber laser cutting machine, the laser power must be increased by approximately 30% (to 6.5 kW or higher) compared to cutting 304 stainless steel of the same thickness to ensure stable penetration and a smooth cut surface.
Why Use Laser Cut Stainless Steel?
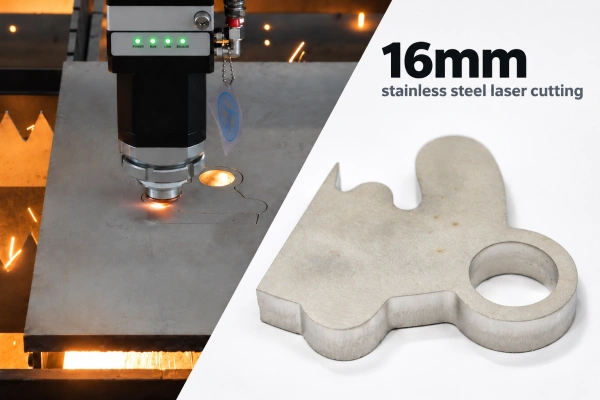
Use fiber laser cutting stainless steel because they are faster, more energy-efficient, and easier to maintain. Fiber lasers operate at a wavelength of approximately 1 micrometer, which is well absorbed by stainless steel, allowing the energy to be concentrated more effectively on the cut. As a result, when processing thin sheets less than 3 millimeters thick, cutting speeds can reach up to about four times that of a CO₂ laser of the same power; for example, a 3-kilowatt machine can cut 6-millimeter-thick stainless steel at a speed of approximately 3 meters per minute.
Fiber lasers have an electro-optical conversion efficiency of approximately 30%, whereas CO₂ lasers typically range from only 10% to 15%, meaning they consume less electricity to perform the same task. Furthermore, they do not require complex mirror optical paths or laser gases; they start up quickly, have fewer potential failure points, and incur lower long-term maintenance costs. The narrow cut and small heat-affected zone also reduce sheet deformation and the need for subsequent grinding.
Conclusion: For common medium- and thin-gauge stainless steel sheets, fiber lasers can achieve higher output and more consistent cutting quality at a lower overall cost, and are therefore gradually becoming the mainstream choice; however, for ultra-thick sheets, the selection must still be based on specific considerations of power, speed, and cost.
Stainless Steel Laser Cutting Thickness and Power
Choosing the Right Laser Power
When laser cutting stainless steel, selecting the appropriate laser power is essential to achieving the optimal balance between cut quality, processing efficiency, and production costs. Too low a power setting may result in incomplete penetration or severe slag buildup on the base material, while too high a power setting can cause overheating, deformation, and burn marks on the cut edge, as well as wasteful spending on equipment, electricity, and gas. Only when the power is perfectly matched to the thickness of the stainless steel can a smooth, burr-free cut edge be ensured, and the equipment’s full processing potential be realized.
Choose laser power based on the stainless steel grade, sheet thickness, assist gas, and your requirements for cutting speed and edge quality. Use the table below to narrow down your options, then confirm the settings with a sample cut before batch production.
Stainless Steel Cutting Thickness by Laser Power
| Laser Power | Reference Cutting Range | Maximum Listed Thickness |
|---|---|---|
| 1.5 kW | 1–6 mm | 6 mm |
| 2 kW | 1–8 mm | 8 mm |
| 3 kW | 1–8 mm | 10 mm* |
| 4 kW | 1–10 mm | 12 mm* |
| 6 kW (34 μm core) | 1–16 mm | 18 mm* |
| 6 kW (75 μm core) | 1–18 mm | 20 mm* |
| 12 kW | 1–25 mm | 40 mm* |
| 15 kW | 1–30 mm | 50 mm* |
| 20 kW | 1–40 mm | 100 mm* |
| 30 kW | 1–50 mm | 70 mm* |
| 40 kW | 5–70 mm | 100 mm* |
| 60 kW | 20–150 mm | 150 mm |
| 80 kW | 20–150 mm | 150 mm |
* Trial-cutting parameter. The source database identifies these settings for sample cutting or small batches and does not recommend them for routine mass production. Reference ranges exclude these trial-cutting entries.
The 1.5–40 kW rows use nitrogen-assisted cutting data; the 60 kW and 80 kW rows use air-assisted cutting data. Two 6 kW fiber-core configurations are shown separately because their listed thickness ranges differ.
Ranges and maxima summarize the thicknesses listed in the database, not guaranteed production limits or minimum cutting capabilities. Confirm the required edge quality and cutting speed for your machine configuration.
Related Products
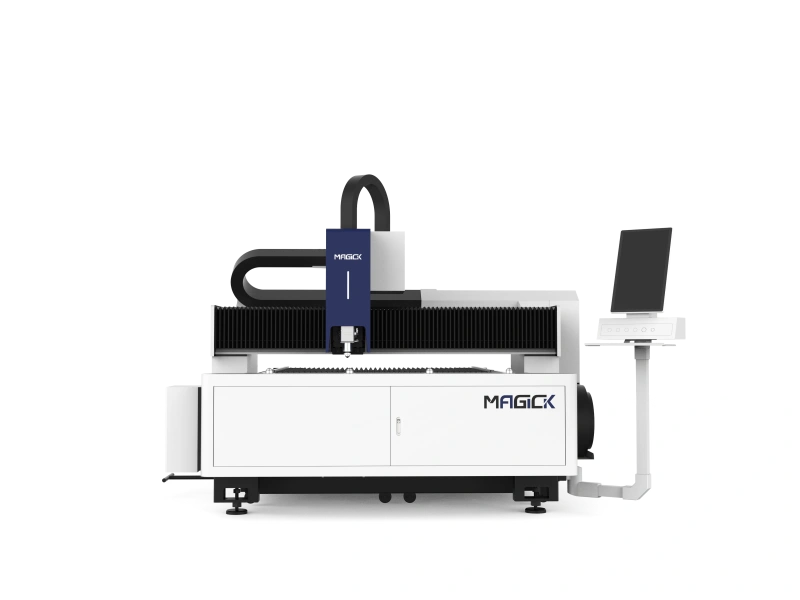
MK-S Single Table Fiber Laser Cutting Machine
A flexible sheet metal cutting solution with an open-table design, suitable for small workshops and diverse stainless steel processing needs.
View MK-S Details
MK-E Exchange Table Fiber Laser Cutting Machine
An exchange table design that reduces loading downtime and supports efficient batch production of stainless steel sheets.
View MK-E Details
MK-TY Tube Laser Cutting Machine
A cost-effective tube cutting solution with a compact layout and reduced end remnants, suitable for light- to medium-duty stainlss steel tube processing.
View MK-TY Details
MK-T2C Dual-Chuck Tube Laser Cutting Machine
A side-mounted dual-chuck design that simplifies tube loading and supports stable cutting for small and medium-sized metal fabrication workshops.
View MK-T2C DetailsRelated Articles
Laser Cutting Steel Sheet: A Practical Guide for Manufacturers
Learn how laser cutting steel sheet works, how to assess 20 mm cutting, edge quality and cost, and how to choose the right fiber laser machine.
Fiber Laser Cutter Buying Guide: Power, Price & Key Specs
Compare fiber laser cutter power, prices and key specs. Find the right configuration and request a tailored quote.
How Does a Laser Cutter Work?
How does a laser cutter work? Learn how laser focusing, assist gas, and CNC motion create precise metal cut.